Chemcote Food and Beverage Coating Solutions
Advanced Anti-Corrosion, Food-Safe and Hygienic Asset Integrity Coatings for Food & Beverage Infrastructure
Protecting food and beverage processing, brewing and dairy infrastructure requires specialised engineering coating systems capable of withstanding constant exposure to aggressive organic acids, high-pressure steam, thermal shock, harsh CIP (clean-in-place) chemicals and continuous moisture. Critical plant assets including process vessels, mixing tanks, flooring, pipework, pumps and concrete bunds face rapid pitting, chemical degradation, concrete erosion and coating breakdown. Without advanced surface protection, equipment failures lead to costly production downtime, non-compliance with health standards and severe risks to food quality and safety.
Chemcote provides industry-leading, Australian-owned protective coating applications, NACE and ACA certified inspections, design specifications and asset refurbishment services across Australia. Chemcote deploys a specialised range of FDA-approved, non-toxic and solvent-free protective coatings engineered to withstand aggressive washdowns while ensuring 100% health safety and regulatory compliance for your customers and products.
The Food & Beverage Corrosion Challenge
Operating food, beverage, dairy and brewing manufacturing facilities presents unique hygienic and structural degradation hurdles:
Aggressive Cleaning Regimes: Frequent high-pressure hot water washdowns, steam cleaning and harsh CIP chemicals (caustic wash and sanitising agents) rapidly erode standard industrial paints.
Chemical Properties of Process Ingredients: Natural food acids, sugars, fats, dairy proteins and beverage ingredients create a highly corrosive micro-environment on processing equipment and floors.
Hygienic & Direct Food Contact Standards: Protective coatings must form an impenetrable, seamless barrier that adheres strongly to metal and concrete without leaching hazardous compounds or flaking into food products.
Downtime & Contamination Risks: Equipment failures compromise product safety, while traditional solvent-based coatings emit hazardous VOC fumes that can taint ingredients during active plant operations.
Why Chemcote? The Technology Advantage
Chemcote shifts the maintenance paradigm by deploying FDA-approved, solvent-free and non-toxic coating technologies engineered specifically for the food and beverage sector. Our specialised systems eliminate hazardous solvent fumes, prevent product contamination and allow fast return to service during tight shutdown windows.
CONVENTIONAL FOOD PLANT PAINTS
- Requires Dry Abrasive Blasting
- Non-FDA Compliant & Leaching Risks
- Fails Under High-Pressure Steam & Thermal Shock
- Hazardous VOC Fumes Taint Food Products
- Extended Production Downtime
CHEMCOTE ADVANCED SYSTEMS
- Surface Tolerant & Solvent-Free
- 100% FDA-Approved & Food-Contact Safe
- Extreme Thermal Shock & CIP Chemical Resistance
- Seamless, Easy-Clean Hygienic Surface
- Rapid Cure & Return to Active Production
Key Technical Benefits
1. FDA-Approved & Non-Toxic Safety
100% solvent-free formulations mean zero Volatile Organic ComOur specialised food-grade linings comply with strict FDA and Australian health standards, providing a completely safe, non-toxic surface that can come into direct contact with food products without leaching or contamination risks. pounds (VOCs), zero fire risk in confined spaces (ballast or cargo tanks) and no biocide leaching into ocean ecosystems.
2. Thermal Shock & High-Pressure Washdown Resistance
Formulated to withstand sudden temperature swings, continuous steam cleaning and daily high-pressure water washdowns without cracking, blistering or losing adhesion to steel or concrete.
3. Zero VOC & Low-Odour Application
100% solvent-free formulations emit zero Volatile Organic Compounds (VOCs) and virtually no odour, allowing maintenance to proceed safely in processing zones without risking product taint or plant contamination.
4. Seamless Hygienic Protection & Chemical Barrier
Creates an ultra-smooth, non-porous finish that resists organic food acids, sugars, caustics and sanitising chemicals, eliminating micro-cracks where bacteria and mould can harbour.
Specialised Food and Beverage Solutions
1. Process Vessels, Mixing Tanks and Silos
Internal re-lining of raw material silos, liquid food storage tanks and mixing vessels using FDA-approved, non-toxic epoxies to deliver long-term corrosion resistance without affecting taste or product purity.
2. Processing Floors, Walkways and Drainage Bunds
Restoring corroded concrete floors, drainage channels and chemical bunds exposed to food acids, thermal shock and heavy forklift traffic. Providing seamless, anti-slip hygienic flooring systems.
3. Pipework, Valves and Fluid Handling Pumps
Protecting stainless steel and cast iron food pumps, slurry valves and liquid distribution pipework against erosion, cavitation and chemical washdown corrosion.
4. CIP Chemical Bunds and Storage Areas
Heavy-duty lining systems for clean-in-place chemical containment bunds, protecting concrete infrastructure against concentrated caustic soda, acid washes and sanitising solutions.
Why Chemcote? The Technology Advantage
Chemcote shifts the maintenance paradigm by deploying solvent-free, wet, rust and oil-tolerant coating technology. Unlike conventional paints, our systems do not require clinically dry or perfectly blast-cleaned steel.

SURFACE PREPARATION
- Ultra High Pressure Water Jetting (UHP)
- Abrasive & Dust-Free Blasting
- Hygienic Surface Washing & Decontamination

SPECIFICATION & INSPECTION
- NACE & ACA Certified Coating Inspectors
- FDA Compliance & Food Safety Audit Verification
- Full QA Holiday Spark Testing & Thickness Verification

COATINGS APPLICATION
- FDA-Approved Tank & Vessel Re-Lining
- Hygienic Anti-Slip Floor Restoration
- Underwater Patching & Composite Reinforcement
Food & Beverage Assets Protected
Asset Category
Specific Applications
Coating System
Processing & Storage Vessels
Mixing Tanks, Fermenters, Product Silos, Storage Vessels, Hoppers
FDA-Approved Food-Grade Epoxy Linings & Non-Toxic Ceramic Coatings
Fluid Handling & Transfer
Product Transfer Pipelines, Valves, Process Pumps, Impellers, Strainers
Non-Toxic Fluid Efficiency Linings & Low-Friction Epoxies
Floors & Drainage
Processing Hall Floors, Packaging Area Walkways, Drain Channels, Plinths
Heavy-Duty Hygienic Concrete Linings & Anti-Slip Flooring
Chemical Containment
CIP Chemical Bunds, Caustic Storage, Water Treatment Tanks, Wash Bays
Chem-Deck, Epo-Chem RF 500 & Chemical Resistant Vinyl Esters
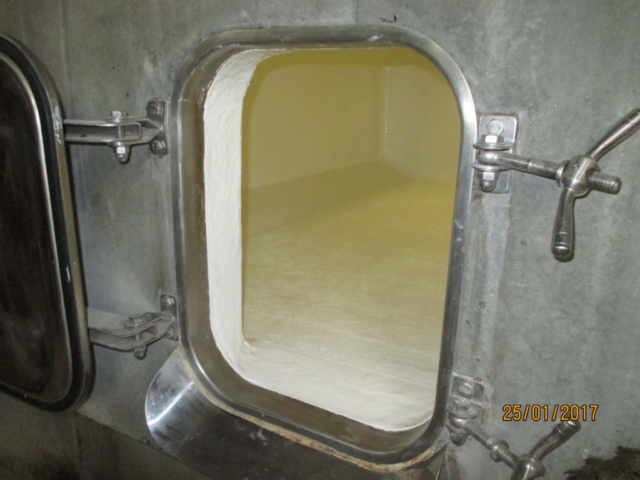
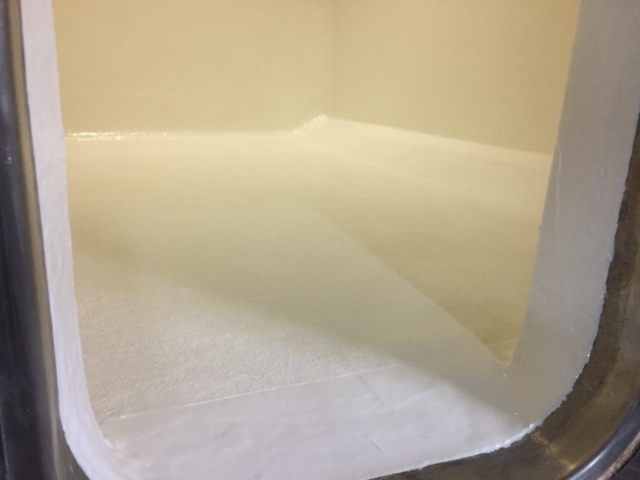
CASE STUDIES
Check out some of the projects we’ve worked on.


Contact Us For Our Food & Beverage Brochure
Gain complete technical specifications, application guides and performance data for our hygienic, food-safe protective systems.

Frequently Asked Questions
Are Chemcote coatings safe for direct contact with food and beverage products?
Yes. Chemcote utilises a specialised range of FDA-approved, non-toxic and solvent-free protective coatings engineered specifically for direct and indirect food contact. They emit zero harmful VOCs and will not leach chemicals into food or affect product taste.
How do Chemcote coatings withstand aggressive CIP cleaning chemicals and steam washdowns?
Our food-grade epoxies and ceramic coatings are formulated to resist harsh Clean-In-Place (CIP) chemicals, including concentrated caustic soda and nitric acid washes, as well as severe thermal shock from continuous hot water and high-pressure steam cleaning.
Can coating repairs be performed without contaminating nearby food production?
Yes. Because our FDA-approved food-grade coatings are 100% solvent-free and virtually odourless, application can take place safely during plant maintenance periods without generating toxic solvent fumes that could taint surrounding ingredients or equipment.
How do protective coatings prevent bacterial growth on processing floors and walls?
Corroded, spalling concrete and cracked paints create microscopic crevices where moisture, food particles and bacteria can thrive. Chemcote applies seamless, non-porous hygienic coatings that eliminate cracks and joints, creating a smooth, easy-to-clean surface that meets stringent health inspection standards.