Chemcote Mining and Mineral Processing Coating Solutions
Advanced Anti-Corrosion, Abrasion Resistance and Asset Refurbishment for Mining & Mineral Infrastructure
Protecting mining, washery and mineral processing infrastructure requires specialised engineering coatings capable of withstanding extreme mechanical abrasion, aggressive process chemicals, high temperatures and severe slurry impacts. Key extraction assets including clarifiers, slurry pumps, flotation cells, launders and chemical containment bunds suffer from rapid metal loss, erosion and structural corrosion. Without advanced surface protection, these harsh operating environments lead to frequent equipment failure, unexpected shutdown delays and escalating maintenance expenditures.
Chemcote provides industry-leading, Australian-owned protective coating applications, NACE and ACA certified inspections, design specifications and asset refurbishment services across Australia. Utilising high-performance ceramic bead-filled epoxies, basalt fibre composites, vinyl ester glassflake series and surface-tolerant epoxies, Chemcote extends the operational lifespan of critical mining infrastructure while improving fluid dynamics and material throughput.
The Mining & Mineral Processing Corrosion Challenge
Operating mineral extraction plants and washeries presents severe structural and mechanical degradation hurdles:
Severe Sliding and Hydrodynamic Abrasion: High-velocity mineral slurries, coke breeze and ore particles cause rapid wall thinning and erosion inside pipework, agitators, launders and pump casings.
Aggressive Chemical and Acid Attack: Exposure to process acids, spent acid lines, ammonia, solvent extraction (SX) reagents and treated process water rapidly degrades conventional industrial coatings.
Heavy Material Build-Up and Friction Drag: Internal surface roughness on fans, blowers and pumps encourages mineral scale accumulation, upsetting dynamic balance and driving up power costs.
Extreme Downtime and Safety Constraints: Mining operations run continuously under tight shutdown schedules, making multi-coat cure delays, hazardous solvent fumes and disruptive dry grit blasting impractical.
Why Chemcote? The Technology Advantage
Chemcote shifts the maintenance paradigm by deploying ceramic bead-filled composites, woven basalt fibre wraps and solvent-free, surface-tolerant glassflake coatings. Unlike standard industrial paints, our advanced systems bond to damp substrates, eliminate scale build-up and provide heavy-duty abrasion barriers without requiring complete plant shutdowns.
CONVENTIONAL MINING PAINTS
- Requires Dry Abrasive Blasting
- Frequent Wear Failures (4-6 Weeks)
- High VOCs & Hazardous Solvents
- Prone to Slurry Build-Up & Imbalance
- Extended Production Downtime
CHEMCOTE ADVANCED SYSTEMS
- Surface Tolerant (Sa 2, WJ-2, St3)
- Ceramic Bead & Basalt Fibre Armour
- Solvent-Free / Low Odour / Zero VOC
- Smooth Low-Friction Anti-Foul Finish
- Rapid Return to Service (76-Hour Cure)
Key Technical Benefits
1. Extreme Abrasion & Impact Protection
Our advanced ceramic bead-filled epoxies (InD-Cote) combined with woven basalt fibre composite wraps (RP 500 AR) provide ultimate resistance against aggressive sliding abrasion and high-temperature coke or ore impact.
2. Improved Material Flow & Balance
Smooth, low-friction topcoats reduce material build-up on fan impellers, agitators and pump volutes, maintaining dynamic operational balance and reducing ongoing power and maintenance costs.
3. Rapid Return to Service & Zero VOC Safety
100% solvent-free, low-odour formulations allow parallel engineering trades to work safely nearby in active plants, achieving full cure and returning critical assets like clarifiers to service within 76 hours.
4. Chemical & Immersed Glassflake Barriers
Our Chem-tect vinyl ester and screened glassflake series (RA 532 / RS 500P) create an impermeable chemical shield over steel and concrete, delivering a design life expectancy exceeding 25 years in immersed process water.
Specialised Mining and Mineral Processing Solutions
1. Clarifier, Thickener and Tank Linings
Heavy-duty internal re-lining for thickeners, clarifiers, spent acid tanks and neutralisation vessels. Utilising surface-tolerant MIO zinc primers (RS 500P) and screened glassflake epoxies (RA 532) to withstand aggressive chemicals and continuous immersion.
2. Pipework, Chute and Slurry Abrasion Armour
Protecting small and large diameter pipe internals, launders and transfer chutes against extreme sliding wear. Deploying ceramic-filled epoxy linings reinforced with basalt fibre wraps to extend pipe operating life from weeks to years.
3. Fan Impeller and Blower Low-Friction Coatings
Applying abrasion-resistant, low-friction linings to fan impellers, dust catchers and scrubbers. The ultra-smooth surface improves laminar air flow, prevents dust build-up and maintains dynamic impeller balance.
4. Pump, Agitator and Multistage Assembly Protection
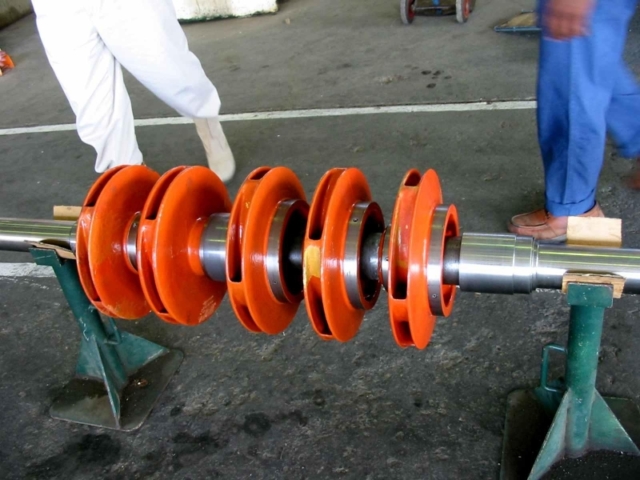
Refurbishing slurry pumps, agitators, multistage assemblies and wear ring lands. Chemical-resistant external barriers safeguard pump cases against hot aqueous ammonia and chemical leaks without risk to internal precision components.
Why Chemcote? The Technology Advantage
Chemcote shifts the maintenance paradigm by deploying solvent-free, wet, rust and oil-tolerant coating technology. Unlike conventional marine paints, our systems do not require clinically dry or perfectly blast-cleaned steel.

SURFACE PREPARATION
- Ultra High Pressure Water Jetting (UHP)
- Abrasive & Glass Bead Blasting
- Hot Washing & Salt Decontamination

SPECIFICATION & INSPECTION
- NACE / AMPP Certified Coating Inspections
- Corrosion Condition Reports & Life Analysis
- Fully Guaranteed Specify, Supply & Apply Solutions

COATINGS APPLICATION
- Ceramic & Basalt Fibre Pipe Armouring
- Confined Space Tank & Clarifier Lining
- Fibre Glass Construction & Concrete Bunding
Mining Assets Protected
Asset Category
Specific Applications
Coating System
Mineral Processing Vessels
Clarifiers, Thickeners, Neutralisation Tanks, Flotation Cells, SX Plants
Epo-Chem RS 500P Primer & RA 532 Screened Glassflake
Slurry & Pipework Systems
Internal/External Pipework, Coke Breeze Conduits, Launders, Agitators
InD-Cote Ceramic Epoxy with Basalt Fibre Wrap & RP 500 AR
Pumps, Fans and Air Handling
Fan Impellers, Slurry Pumps, Multistage Pump Assemblies, Scrubbers, Blowers
Chem-tect RB 300 Series Glassflake & RP 500 Low-Friction Topcoat
Infrastructure and Containment
Concrete Secondary Bunds, Process Floors, Pontoons, Structural Steelwork
Heavy-Duty Concrete Epoxy Linings & Impermeable Vinyl Esters
CASE STUDIES
Check out some of the projects we’ve worked on.


Download Our Mining & Mineral Processing Brochure
Gain complete technical specifications, application guides and performance data for our mining, mineral extraction and washery protective systems.

Frequently Asked Questions
How do Chemcote coatings withstand aggressive sliding slurry abrasion inside pipework and chutes?
We deploy specialised ceramic bead-filled high-temperature epoxies (InD-Cote) reinforced with an external wrap of woven basalt fibre and top-coated with RP 500 AR. This composite structure provides extreme mechanical hardness and toughness, extending pipe life from 4 weeks to well over 9 months in high-wear abrasive environments.
Can Chemcote re-line thickeners and clarifiers during tight plant shutdowns?
Yes. Our solvent-free, low-odour Epo-chem RA 500 series utilises surface-tolerant primers (RS 500P) and fast-curing screened glassflake barriers (RA 532). Because it emits zero VOC fumes and cures rapidly, complete clarifier re-lining projects can be completed, tested and returned to active service in as little as 76 hours.
How does applying low-friction coatings to fan impellers reduce operating costs?
Uncoated fan impellers operating in mineral extraction plants suffer from dust accumulation and non-uniform material build-up, causing severe dynamic imbalance and bearing wear. Applying our low-friction 500 Series lining creates an ultra-smooth finish that maintains laminar air flow, prevents build-up and preserves rotational balance.
How does Chemcote protect pump assemblies exposed to hot chemical environments?
For multistage pumps exposed to aggressive aqueous ammonia or process chemicals at elevated temperatures, Chemcote applies complete external barrier systems over the pump case, coupling guard, channel base frame and motor. Surface-tolerant formulations allow full protection without abrasive blasting risk to precision internal components.