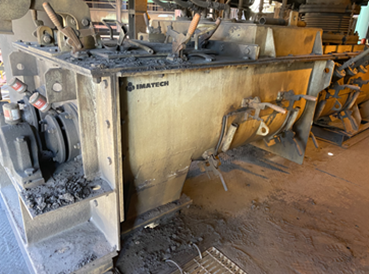
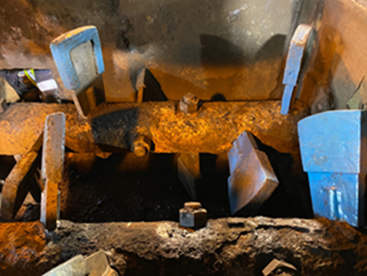
Condition of surface before mechanical preparation
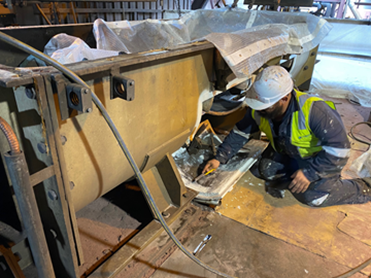
RB 364 applied to spot abrasive blasted surfaces
Pugmill externals
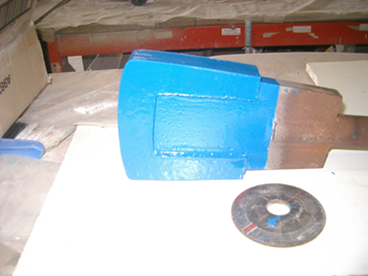
Coating with InD Cote
OVERVIEW: Chemcote’s specialist team mobilised to site to deliver a multiple layer protective coating system that would return the asset to working condition within 24 hours. Abrasion resistant coatings were applied to the pugmill and paddles over a 12 hour period during plant shutdown, with 12 hours allocated for curing.
50-70°C 10-40μm abrasive particles from the dust catcher are disposed of in the pugmill and combined with water to suppress the dust creating an abrasive sludge
SUBSTRATE
Steel Substrate
CHALLENGE
Deliver an operational multi coat abrasion resistant coating system within 24 hours
SOLUTION
Thorough surface preparation prior to the application of multiple layers of abrasion resistant coatings. Spot abrasive blasting to minimise disruption to surrounding trades.
SCOPE
Pugmill Internals Spot abrasive blast localised areas. Apply of 1 coat of fast curing Chem-tect™ RB 364C to areas where required Use chopped strands and where deep pitting existed to provide a smooth even profile Apply 2 coats of Chem-tect™ RB 364CS to 1,000μm Conduct QA, DFT and high voltage spark test to ensure continuity at required voltage
Paddles Abrasive blast to AS 1627.4, Class 2.5 with a minimum 75μm profile. Apply 1 coat of Epo-chem™ RW 500 to a nominal thickness of 500μm to ensure no transparent areas Complete casting application 1 coat of InD-cote™ to 6000 micron DFT to the load and back faces
Chemcote’s solution has extended the life of this asset by 12-24 months, and delivered a 30% improvement in functioning. Continuous high performance is guaranteed until our review at the next planned outage.
Patrol boat in slipway for refit Protection against abrasive blasting damage Application of RB364 Tube internal lining complete Overview: The half-life refit of critical components
Pitting corrosion near shaft landing After first abrasive blasting After 2nd Abrasive blast holes were found requiring composite reinforcement Filling void in difficult to reach