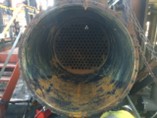
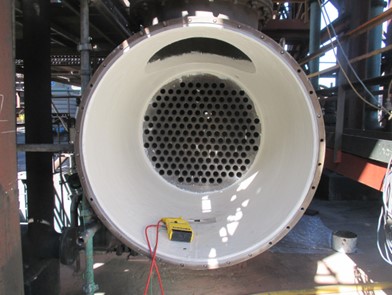
OVERVIEW: The Leading Steel Manufacturer had a preheater in service for a number of years with previously applied coating failing due to poor coating selection and surface preparation and was after a coating to extend service life.
Work had to be completed during a short shutdown duration with only 60 hours allocated for coating application.
Leading steel manufacturer has a preheater in service for a number of years with previously applied coating failing due to poor coating selection and surface preparation. Weld repairs to shell plate were carried out 4 years prior due to the corrosion allowance exceeding parameters.
Engineer was after a coating to extend service life. Work had to be completed during a short shutdown duration with only 60 hours allocated for coating application. Arrangements were made overnight to mobilise the site first thing the following morning.
SOLUTION
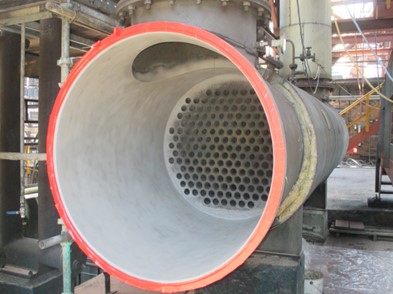
We recommended RB 332, glassflake filled vinyl ester, for its quick cure time, low moisture vapour transmission rate, and excellent corrosion and electrical isolation protection in wet environments. This coating system provides excellent corrosion/erosion resistance.
SCOPE
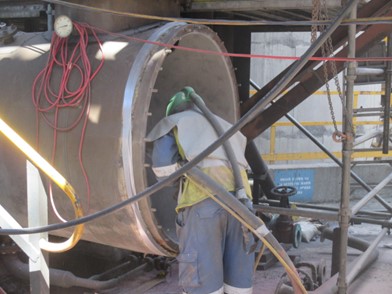
Abrasive blasting to remove dense residue
Potassium Ferrous Cyanide to determine surface cleanliness
Grinding and weld repairs to perforations 1st coat of RB 332 hand applied
DFT checks done after first coat and pit filling Top coat applied
As a result of the fast cure and good project management, the preheater was back into service on time despite various delays. Coating was completed to client’s expectations and future scheduled inspections will ensure long term protection.
Patrol boat in slipway for refit Protection against abrasive blasting damage Application of RB364 Tube internal lining complete Overview: The half-life refit of critical components
Pitting corrosion near shaft landing After first abrasive blasting After 2nd Abrasive blast holes were found requiring composite reinforcement Filling void in difficult to reach