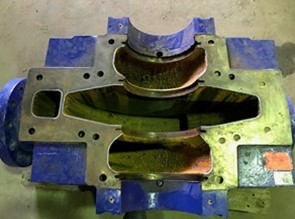
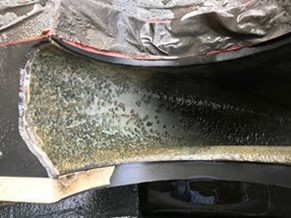
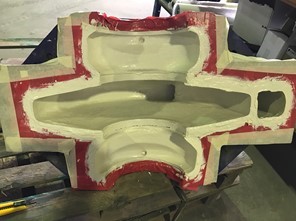
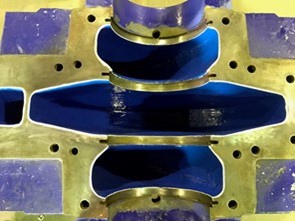
OVERVIEW: A customer was looking for a longer term solution to a corrosion erosion issue. Glass flake filled coatings provide excellent insulating properties against corrosion and the ceramic filled epoxy provides exceptional protection against erosion. The customer has found the pump now functions more efficiently when in use consuming less power allowing a payback period of the entire refurbishment to be only 14 months.
The client’s pump had dropped off in efficiency. This was due to the combination of corrosion and mechanical fatigue. The client was looking to improve efficiency and reduce power consumption.
SOLUTION
After 25+ years in service the substrate was heavily contaminated with metallic salts. This required heat treatment and a number of abrasive blasts to reduce salts below 25ppm. We then recommended the application of 2 coats of RB 332; a glass flake filled vinyl ester providing an excellent corrosion barrier and long term protection. We then applied 2 coats of RB 300GL to enhance fluid efficiency in turn reducing power consumption.
SCOPE
Strip and assess
Manufacture template to ensure mating faces match
Grind rebates on all flanged faces, allowing the coating to be applied on the flange face preventing future crevice corrosion
Protect critical dimensions
Abrasive blast and treat to reduce metallic salts by hot washing and re-abrasive blast
Pump repairs were achieved and by coating with RB 300, future corrosion is prevented with a reduced amount of friction through composite technology. The pump now functions more efficiently when in use and consumes less power, which led to carbon credits and greenhouse gas reduction. The payback period of the entire refurbishment worked out to be only 14 months.
Patrol boat in slipway for refit Protection against abrasive blasting damage Application of RB364 Tube internal lining complete Overview: The half-life refit of critical components
Pitting corrosion near shaft landing After first abrasive blasting After 2nd Abrasive blast holes were found requiring composite reinforcement Filling void in difficult to reach